What you save on the coating, you pay for in downtime.
Two lots with the same specification can have different lives in the field — and the difference does not show on the part: color, gloss and thickness look the same. What separates one from the other is whether the alloy and the layer were measured and recorded. Here every lot ships with a report and an alloy controlled by X-ray, under ISO 9001:2015.
to red rust
controlled by XRF
founded in 1964
BSI · FS 517766
and traceability
Services in order of technical demand.
Every electroplating process runs with the bath analyzed in-house, the coating measured and the test recorded. Full index → What is electroplating →
NanoGalv®
Nanometer-scale layers alternating zinc and nickel: a defect makes corrosion travel between the layers instead of going down to the steel. From 10 µm, it passes 10,000 h to red rust — test by Modumetal, the technology licensor. It stays within the standard thread tolerance — no re-tapping.
Zinc-Nickel
Alloy controlled between 12 and 16% nickel, verified by X-ray on every lot — the range that secures salt spray above 1,000 hours.
- White trivalent1,000 h+
- Black trivalentaesthetic + protection
- Solar energy1,500 h
Xylan®
Low-friction, sealing coating, applied alone or as a topcoat over zinc-nickel in offshore environments. PPG (Whitford) approved applicator.
- Xylan 107015–25 µm · −195 to +260 °C
- Zn-Ni + Xylan® 1070over 3,500 h · B117
- Dynamic friction0.047 · G99
Cadmium
Yellow and olive drab chromate, plus low-hydrogen-embrittlement (LHE) cadmium for aerospace use. Process approved by TechnipFMC.
- Yellowcl. 12 type II · 1,000 h
- Olive drabcl. 12 type II · 1,000 h
- LHElow embrittlement
Alkaline zinc
Trivalent zinc with the market’s main passivations and friction modifiers, including MacDermid’s Finigard line.
- White / yellowtrivalent
- SealersMacDermid Finigard
Phosphate
Adhesion base for paint and organic coatings, and manganese phosphate for break-in and oil retention.
- Zinc phosphatepre-paint
- Manganese phosphateanti-galling
Hydrogen embrittlement relief
Hydrogen relief between 150 °C and 250 °C, in ovens with uniformity survey (TUS) and traceable thermocouple calibration — a requirement for high-strength parts.
- Ovens 02 · 03TUS + SAT 2025
- Recordcurve per lot
Blasting
Surface cleaning and preparation before coating, with no ferrous contamination on stainless parts.
- Stainless shotuniform finish
- Aluminum oxideanchor profile
Coating and alloy measurement by X-ray (XRF).
In 2025 we installed the Skyray Thick200 XRF to control the zinc-nickel and nanostructured zinc-nickel alloy inside our own line. The instrument has spare capacity — and now we run the test for third parties to Petrobras requirements: you send the part, you receive the report of thickness and composition.
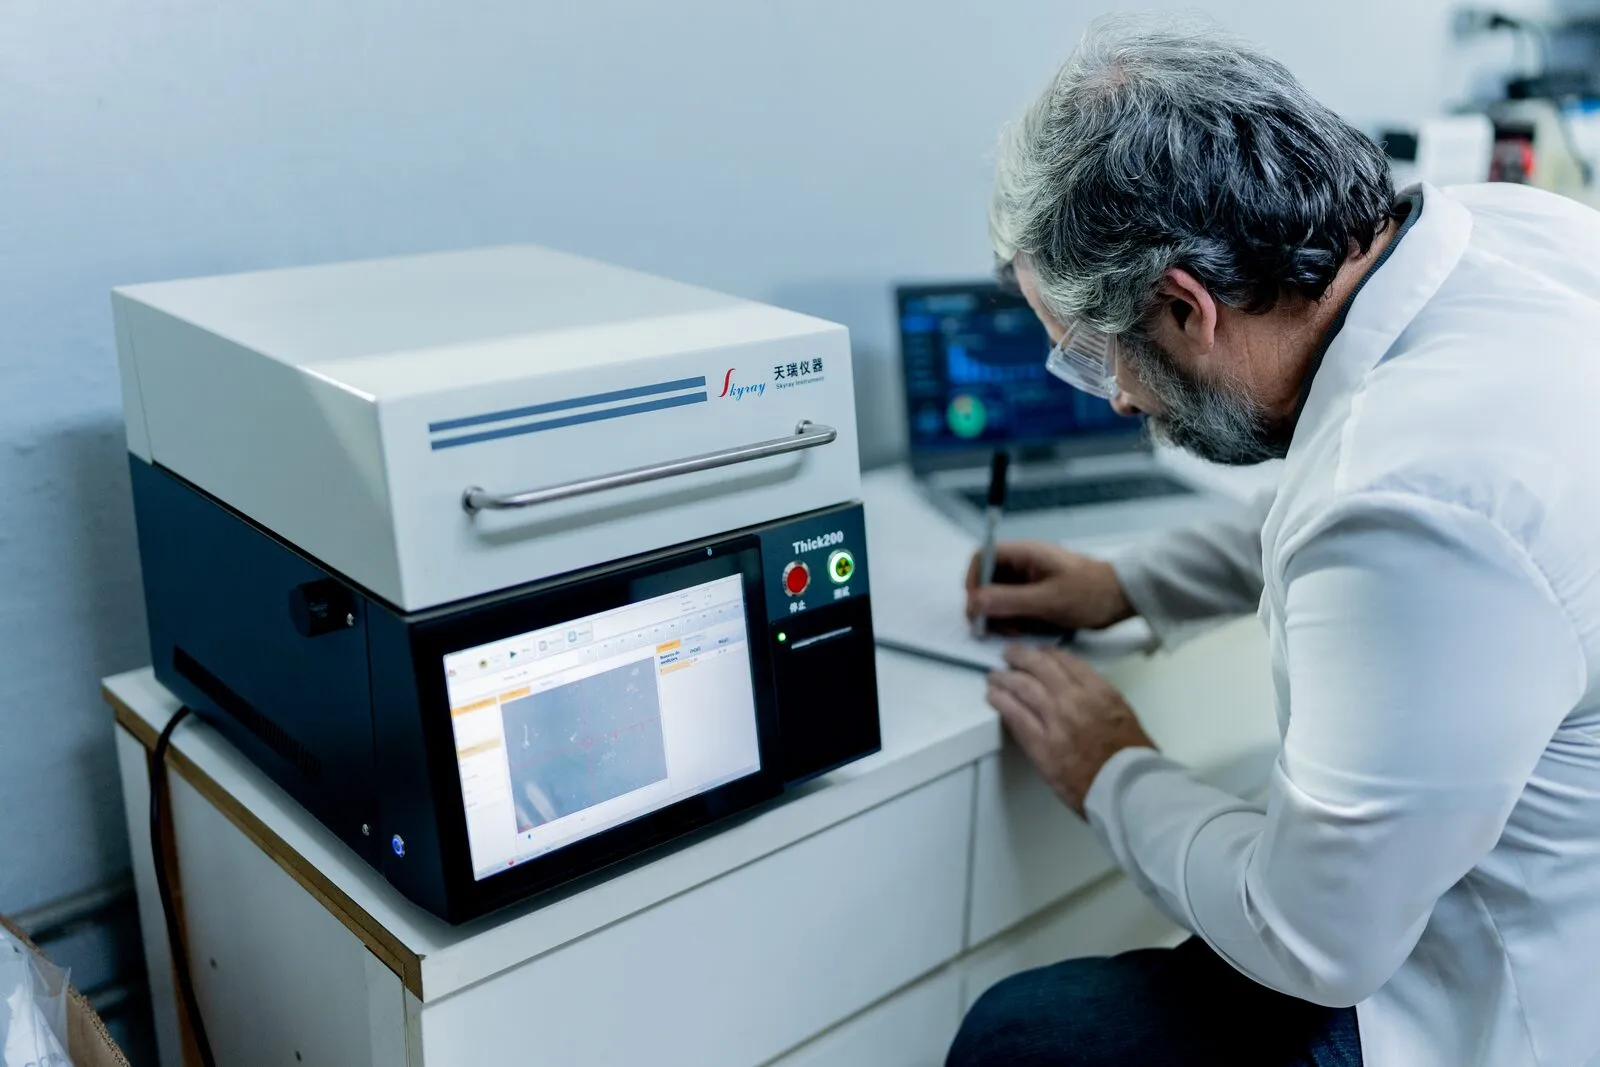
Coating and alloy reading on the XRF · in-house laboratory, Guarulhos
Why the alloy matters
Only between 12 and 16% nickel does zinc-nickel deliver salt spray above 1,000 hours. Outside the range, the coating looks compliant and fails in the field.
Wet-chemistry bath analysis
A complete laboratory for every bath, with no reliance on a supplier’s weekly analysis. Every replenishment is recorded in the system.
Corrosion testing
Preece and Kesternich, analytical balance and Hull cell with determination of the electrolyte efficiency factor.
Where our coating is critical.
Each segment has its own set of standards, approvals and documentation — and we deliver all three.
Oil & Gas and Subsea
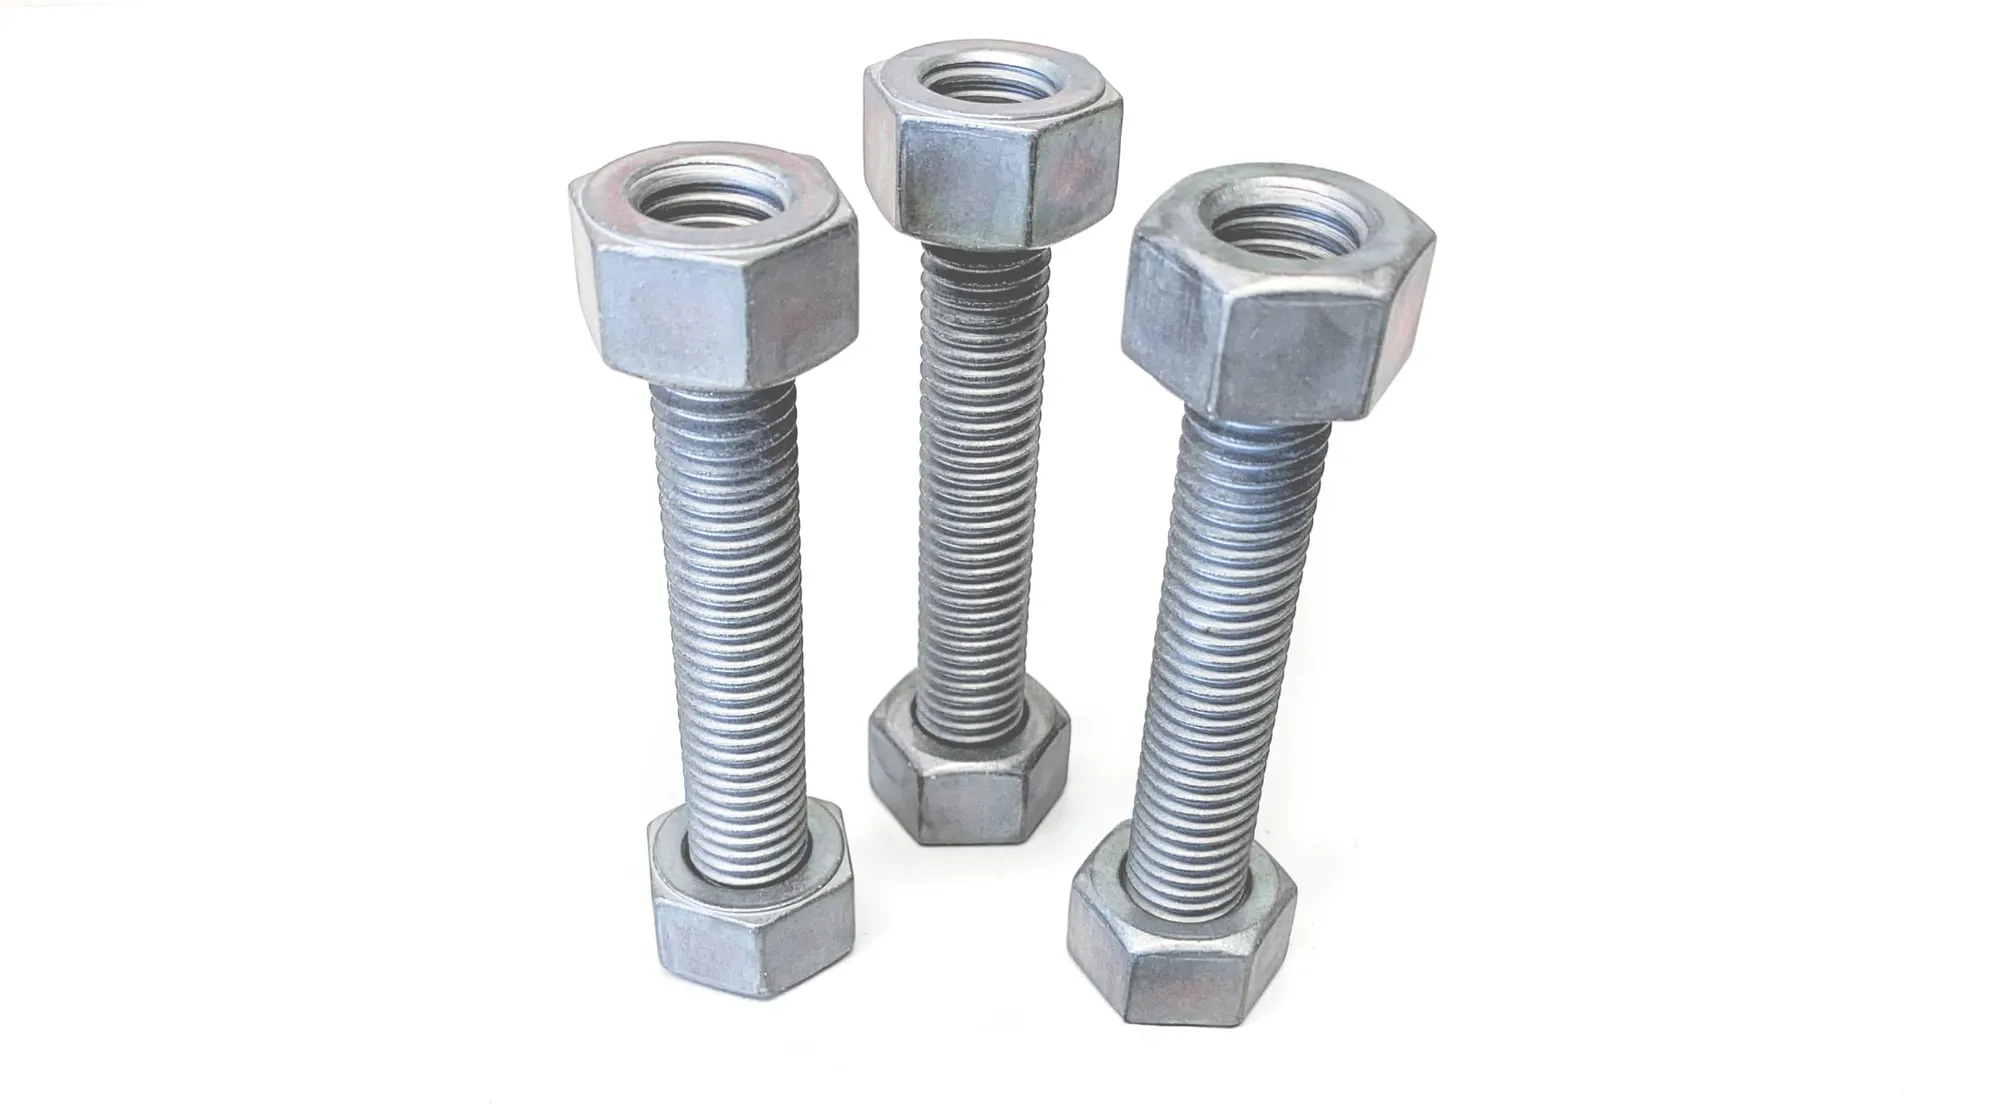
NanoGalv® and Xylan® for fasteners, studs and subsea components. In subsea there is no cheap maintenance: the coating decides whether the joint opens on the first torque.
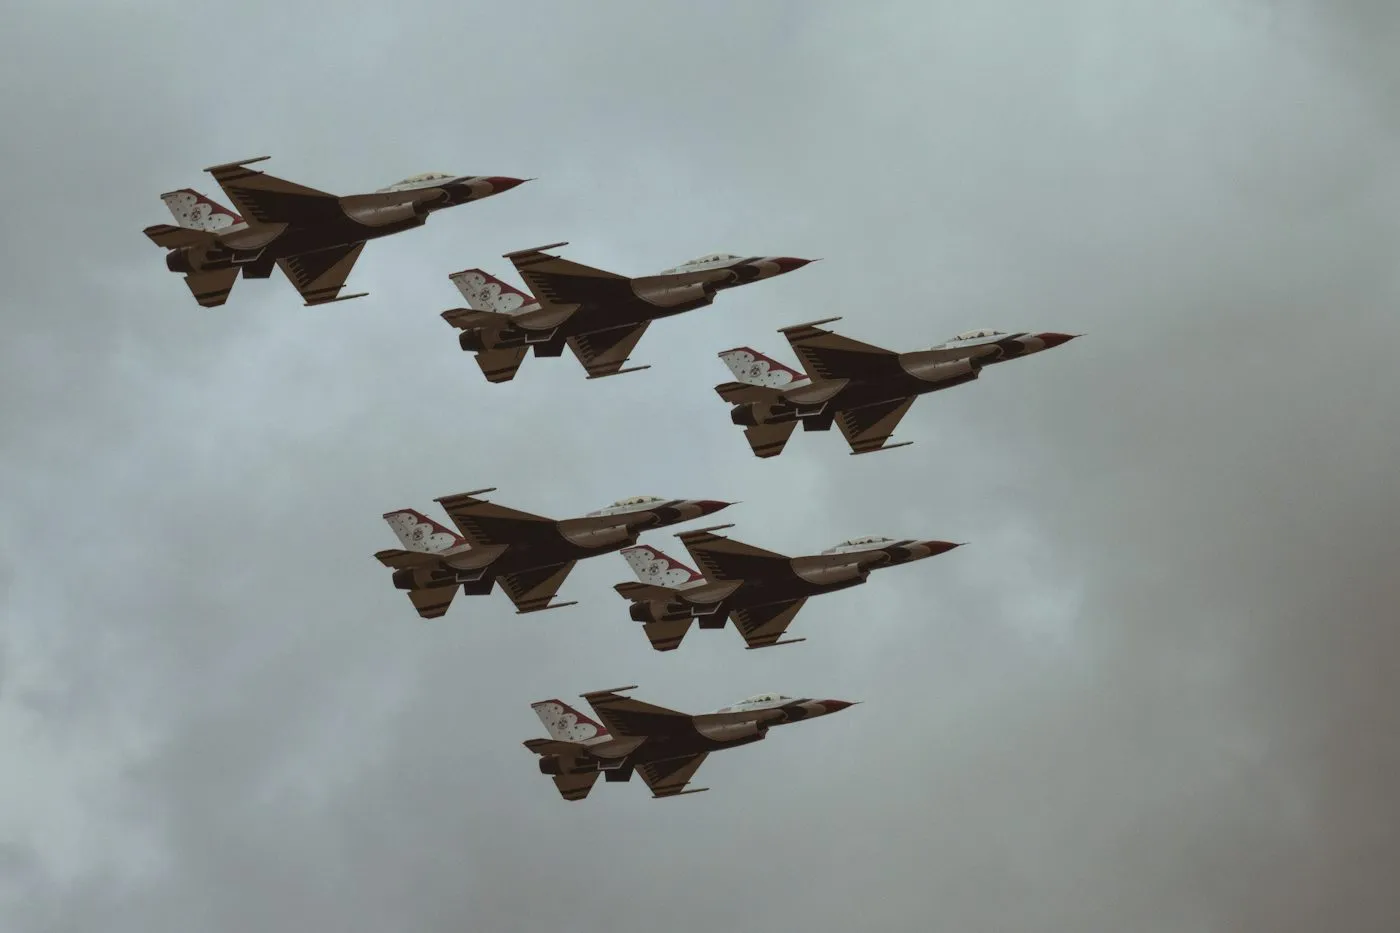
Aerospace & defense
Low-hydrogen-embrittlement cadmium (LHE) and hydrogen relief in a calibrated oven, with the traceability the sector demands.
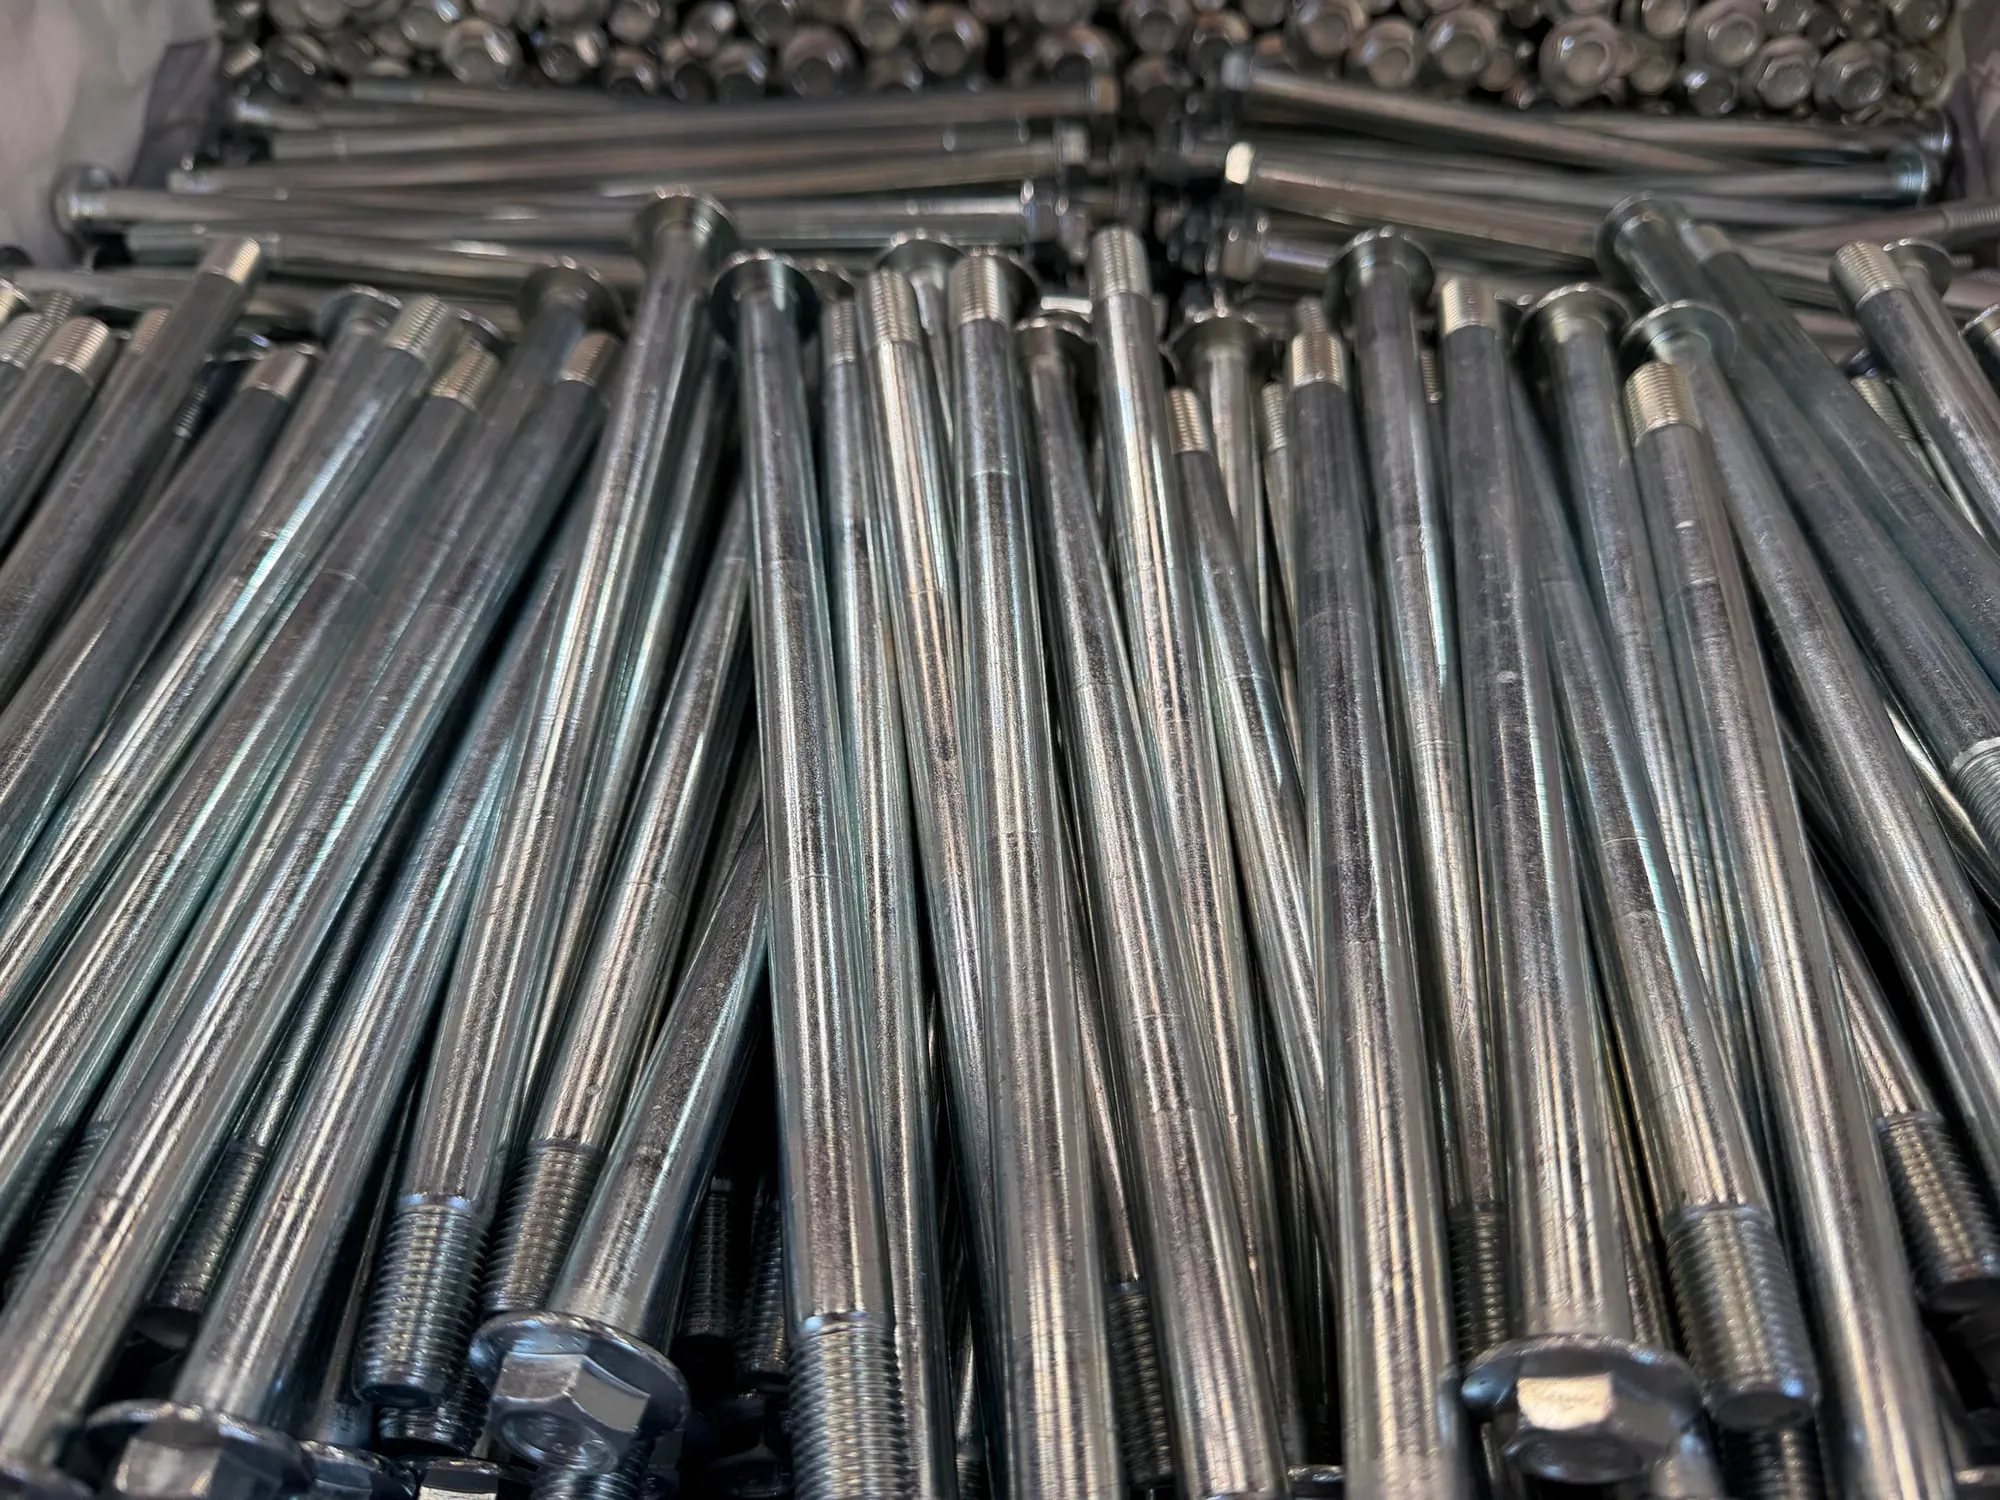
Automotive
PPAP development, CQI-11 compliance and quality Core Tools. Alkaline zinc and Zn-Ni with Finigard sealers and friction modifiers.
Documentation ready for your audit.
Certificates, coating approvals and oven calibration for download.
What drives us.
To make critical equipment last longer and stop less. In sectors where failure is not an option — aerospace, oil & gas and subsea — we deliver the complete corrosion-protection solution: the right technology, the finished fastener and the measured proof.
To be recognized as the reference in coating technology for high-criticality, high-value applications — specified by name by the equipment manufacturers that cannot afford to fail.
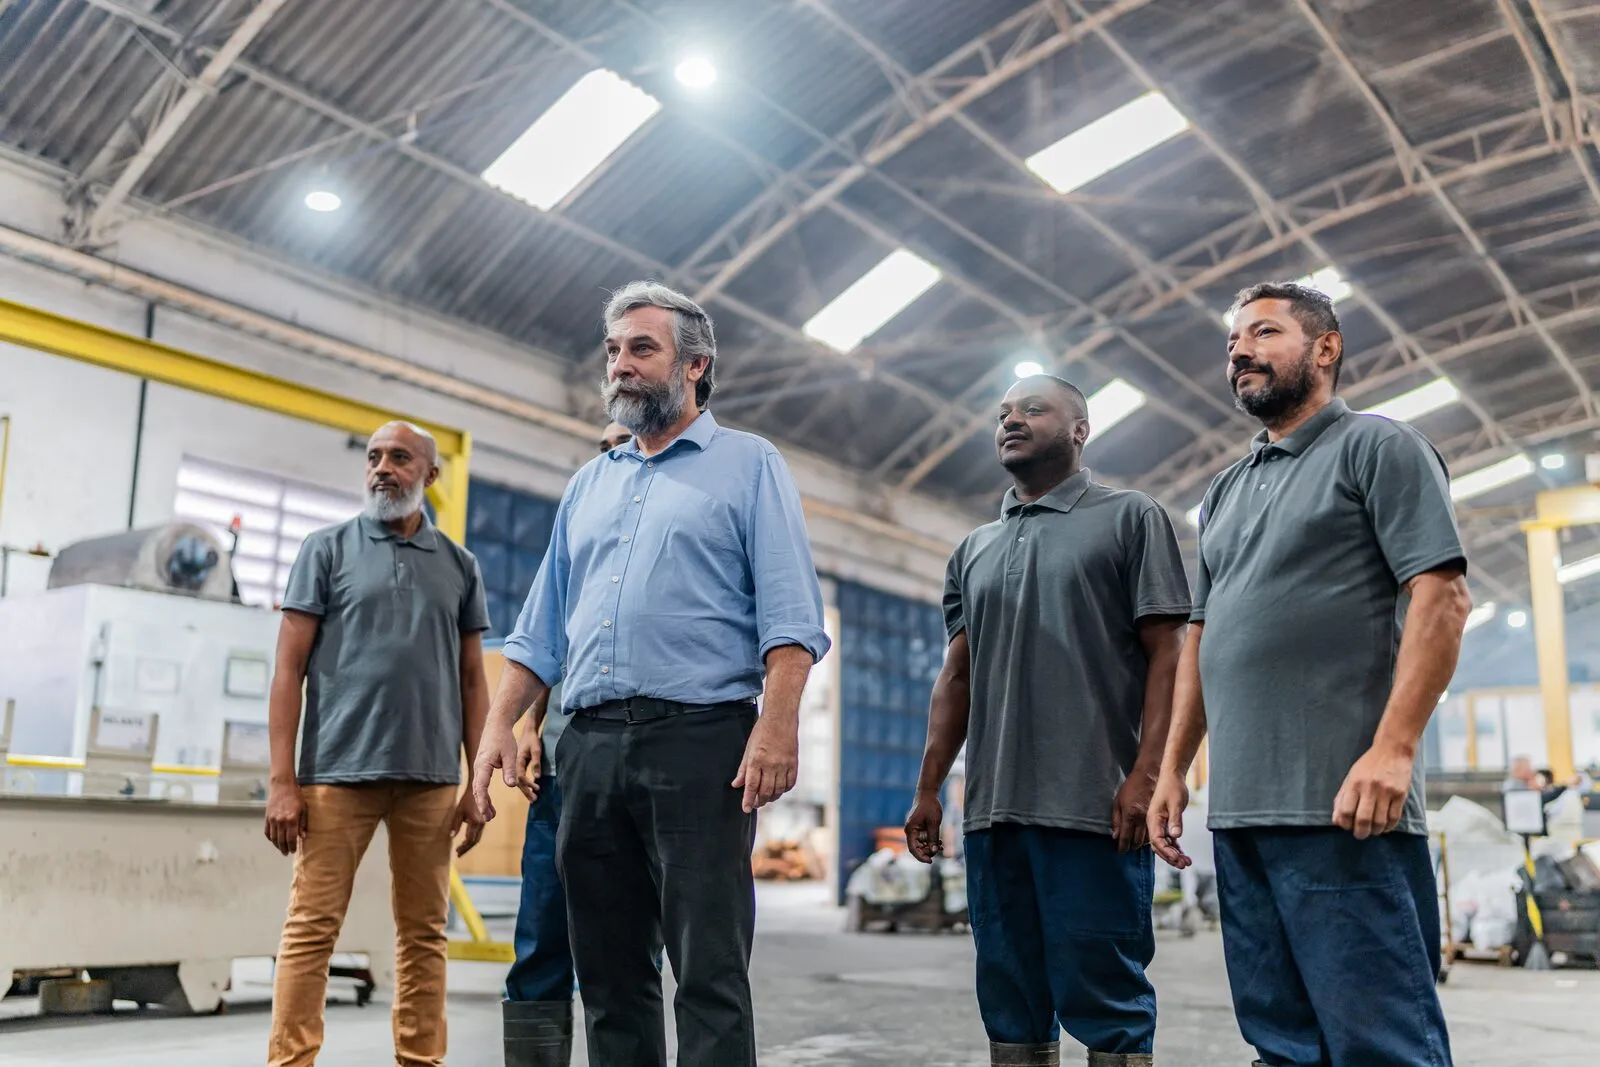
Floor meeting · process indicators and the previous shift’s nonconformities
A controlled process is people who control it.
The layer that passes salt spray comes off a line run by our own team, with a floor meeting every shift, the bath analyzed in our own laboratory and the lot record made by the person at the tank — not by a spreadsheet filled in later.
same family
of the line
of indicators
Recorded training
Operators trained and requalified under the ISO 9001:2015 QMS, with a record by role and process.
Whoever answers knows the line
Our sales team answers with the process in hand: whoever quotes has access to the lot history and to the laboratory.
The operation, as it is.
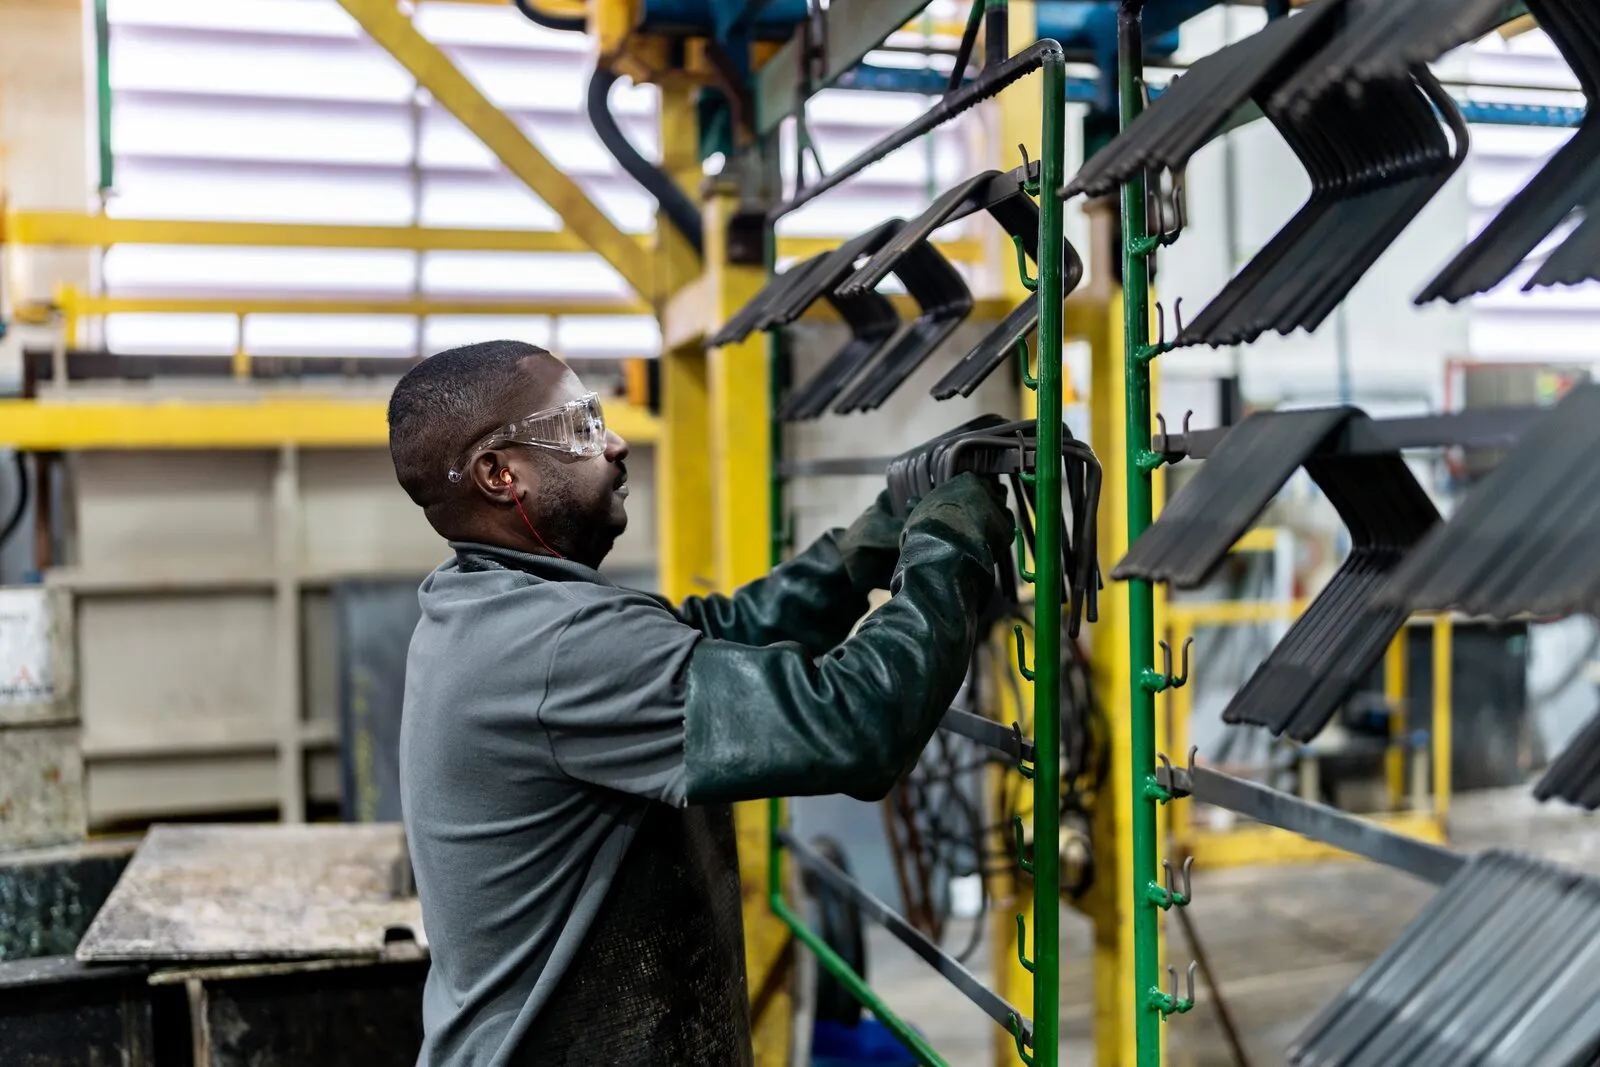
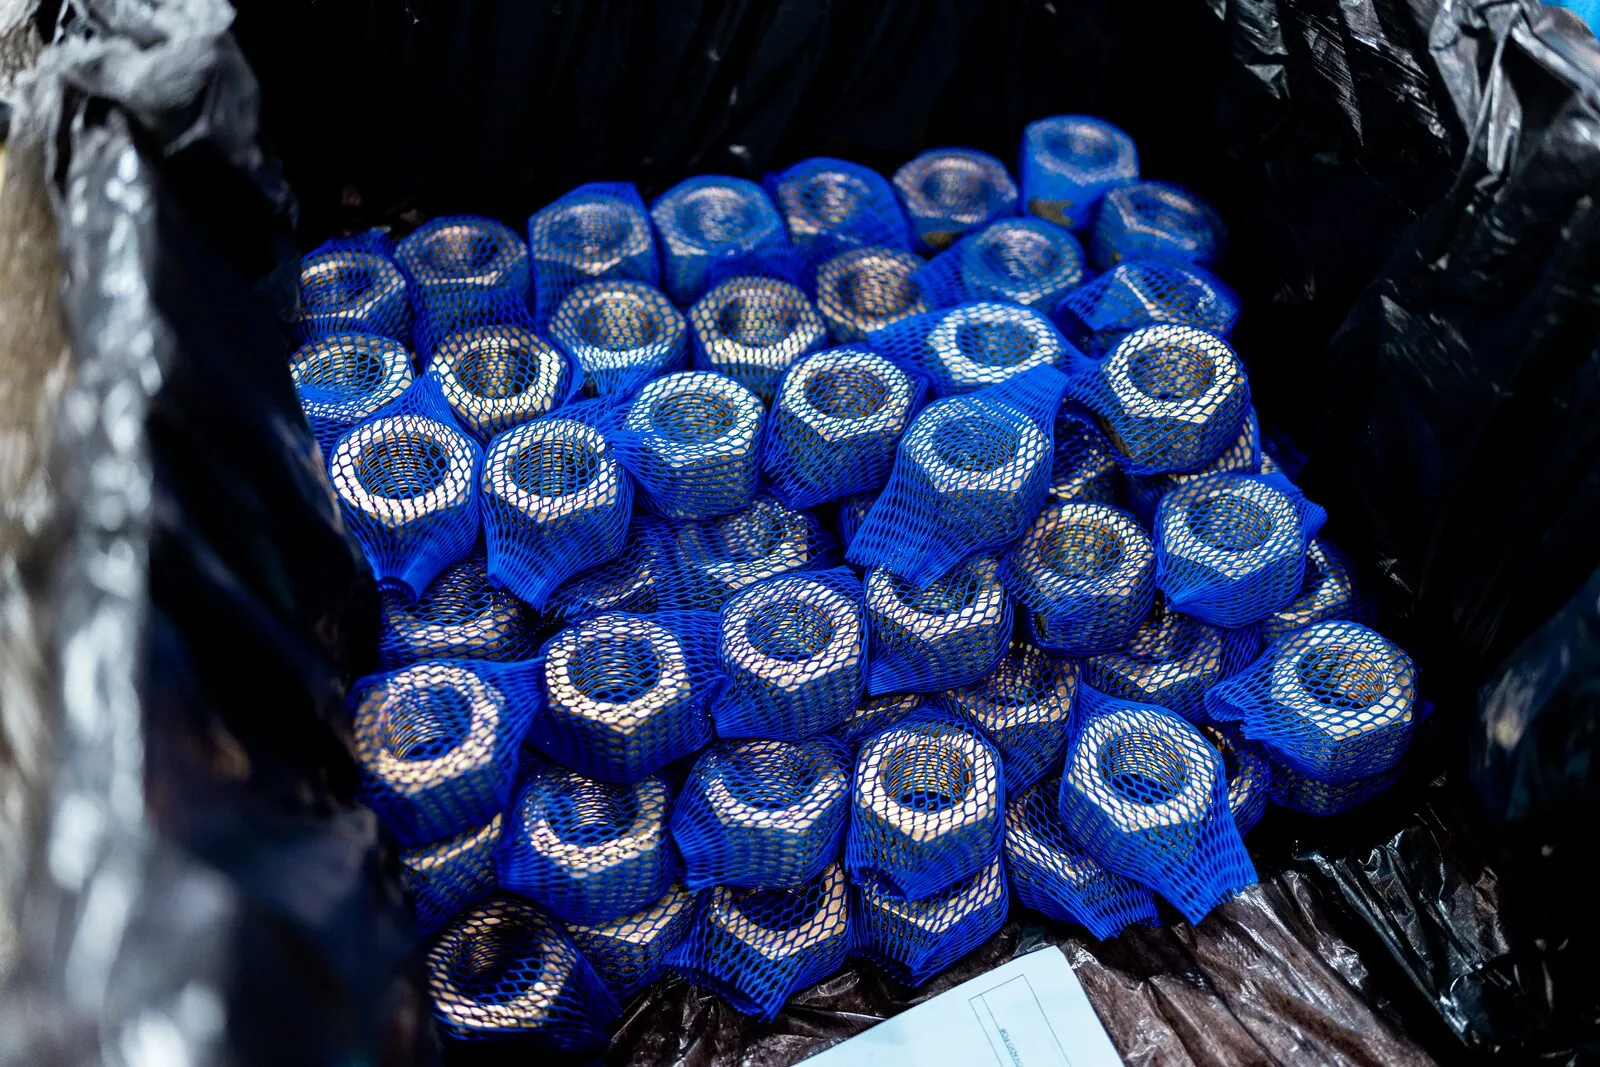
Line, laboratory, finished part and the team behind it. What is on Instagram is the same factory that receives your part.
The drawing and the standard. We specify the rest.
With the part drawing and the coating standard, the reply comes with system, class and thickness — not just a price. Quotation page →
Technical drawing of the part
Geometry, base material, hardness and heat treatment — the drawing tells whether the part goes in a barrel or on a rack and whether the fastener needs hydrogen embrittlement relief.
Coating standard
ASTM B841, ASTM B766, AMS-QQ-P-416 or your end customer’s specification. The standard already defines class, thickness and test.
Four details are enough
Without a drawing and a standard, our sales team quotes from the material thickness, the bath wanted, the part type and the thickness in microns.
Request a quotation
Our sales team replies within 1 business day. Have a drawing and a standard? Say so in the details and send the file by e-mail or WhatsApp — the form takes no attachments. For laboratory testing, choose “X-ray (XRF) measurement”.
We use this data only to answer your request. Submission is processed by Web3Forms (United States), which forwards it to vendas@sapucaia.com. A copy is recorded in our sales system, on a server in Brazil, and the anti-spam check is run by Cloudflare.
Or reach us directly: WhatsApp 11 2603-6759 · vendas@sapucaia.com
What specifiers usually ask.
What is the difference between conventional zinc-nickel and NanoGalv®?
Conventional zinc-nickel deposits a continuous layer and meets ASTM B841 with a 12 to 16% nickel alloy. NanoGalv® modulates the current to deposit multiple nanolayers, creating barriers in series — a defect makes corrosion travel between the layers instead of going down to the steel. The coating conforms to ASTM B1025-25, and the test by Modumetal, the licensor, measures to ASTM B117: it passes 10,000 hours to red rust from 10 µm, 7,300 hours at 8 µm and 4,000 hours at just 5 µm. On that base, Xylan® adds an organic barrier. Conventional is the base of the portfolio; NanoGalv® is the upgrade for when stopping is not an option.
Does NanoGalv® change the thread on my part?
No. The layer stays within the standard thread tolerance, with no need to re-tap and no change to the customer’s design.
Am I locked into a single supplier if I specify NanoGalv®?
No. NanoGalv® is an upgrade: conventional zinc-nickel, available from multiple suppliers, remains the base of the portfolio and an alternative for non-critical items.
Does Sapucaia measure coating thickness on third-party parts?
Yes. The laboratory measures coating thickness and alloy composition by X-ray fluorescence (XRF) to Petrobras requirements, with a report issued. External tests are run with standards calibrated by an ISO/IEC 17025 accredited laboratory.
Why must the zinc-nickel alloy stay between 12 and 16% nickel?
It is the range set by ISO 4042, and it is what sustains resistance above 1,000 hours of salt spray. Outside the range, the coating looks compliant and fails in the field. That is why the alloy is checked by X-ray during production, not only at final inspection.
Why does a fastener need hydrogen embrittlement relief?
Electrochemical processes generate ionic hydrogen that diffuses into the metal and causes internal stress, embrittlement or hydride precipitation. Relief is done right after plating, between 150 °C and 250 °C, in ovens with uniformity survey and traceable calibration to API Specification 6A, ISO 10423 and CQI-9.
What we published on the blog.
AI and automation in electroplating: Sapucaia on the EntreCamadas podcast
Juan Victor, director of Sapucaia, is the guest on episode #08 of EntreCamadas, a Brazilian surface-finishing podcast, talking about artificial intelligence and automation in electroplating.
Zinc or manganese phosphate: how to choose the right treatment for each part
Zinc phosphate prepares the part for paint and for oil protection. Manganese phosphate resists wear and galling. See how to choose in three questions.
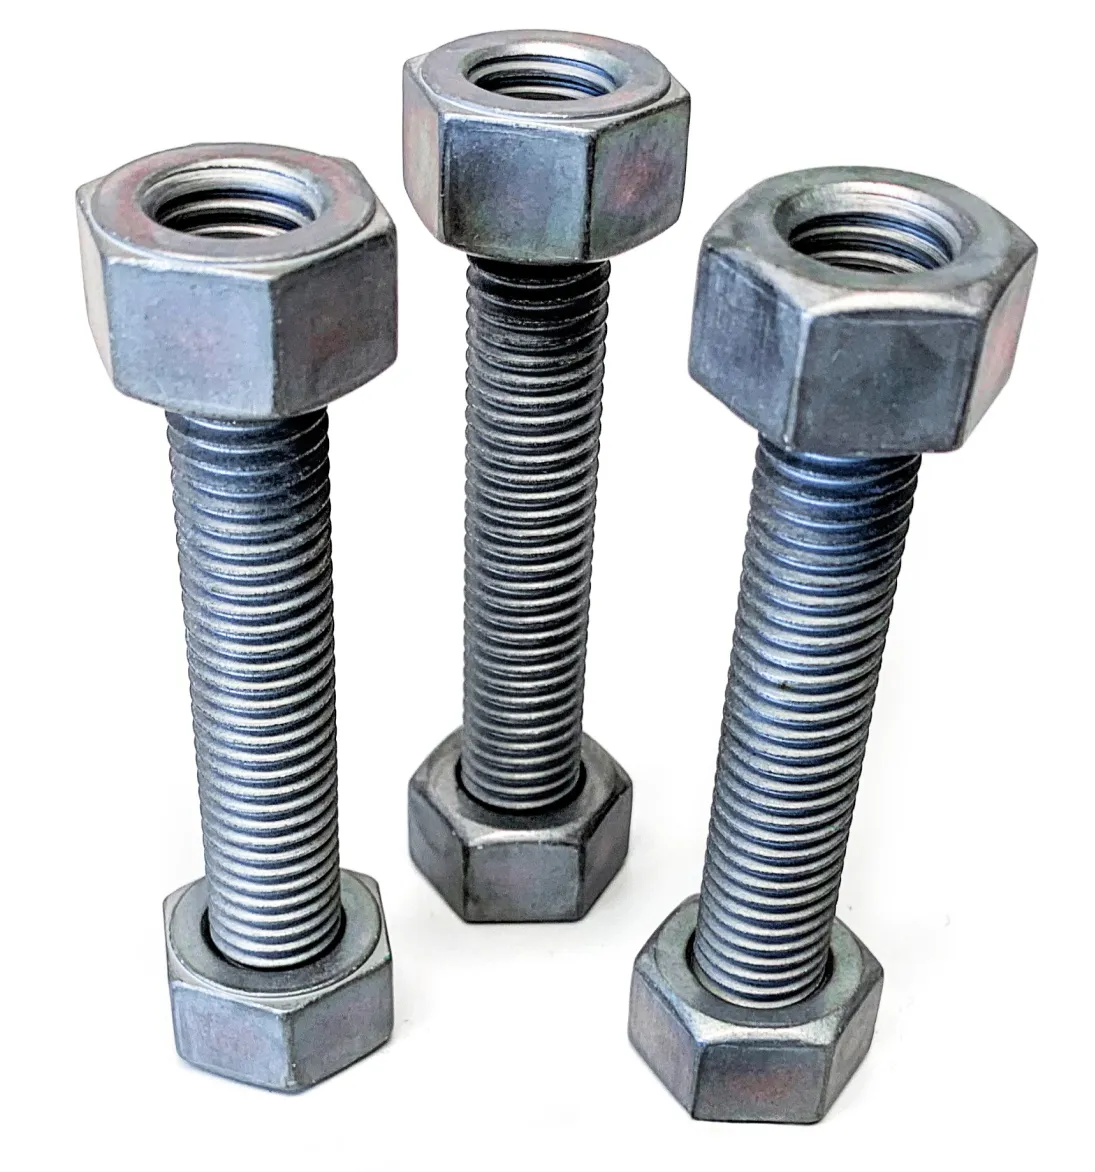
The Equatorial Margin: a new frontier, and the fastener that will go there
Petrobras has twice confirmed oil at the Morpho well, in the Foz do Amazonas basin. Across the border, Guyana shows what comes next — and what the specification asks of the fastener.