Zinc-nickel for solar energy
Panel structure spends 25 years outdoors, with fasteners nobody will replace. The controlled process reaches 1,500 hours of salt spray.
Photovoltaic structure fastening is a peculiar case: the part is cheap, the installation is very expensive to redo, and the asset stays exposed for decades. The cost of the coating is irrelevant next to the cost of going back up on the roof.
For that profile, we take zinc-nickel to the limit of the process — alloy in the high range, passivation and sealer — reaching 1,500 hours in salt spray testing.
Three controls sustain that number, and all of them belong to the process, not to final inspection: the alloy measured by X-ray fluorescence during production, the bath temperature tracked, and the sealer applied to specification. Out of range, the coating leaves with the same look and half the life.
A baseline helps with sizing: electrolytic zinc sits between 200 and 300 h of salt spray, and the bare zinc-nickel base runs from 900 to 1,000 h. For structure that spends 25 years outdoors, the gap between those levels is what decides whether there will be maintenance along the way.
Technical data
- Salt spray
- up to 1,500 h
- Alloy
- 12 to 16% nickel
- Application
- Panel fasteners and structure
- Standard
- ASTM B841 · ISO 4042
The applications that come here.
Photovoltaic structure fasteners
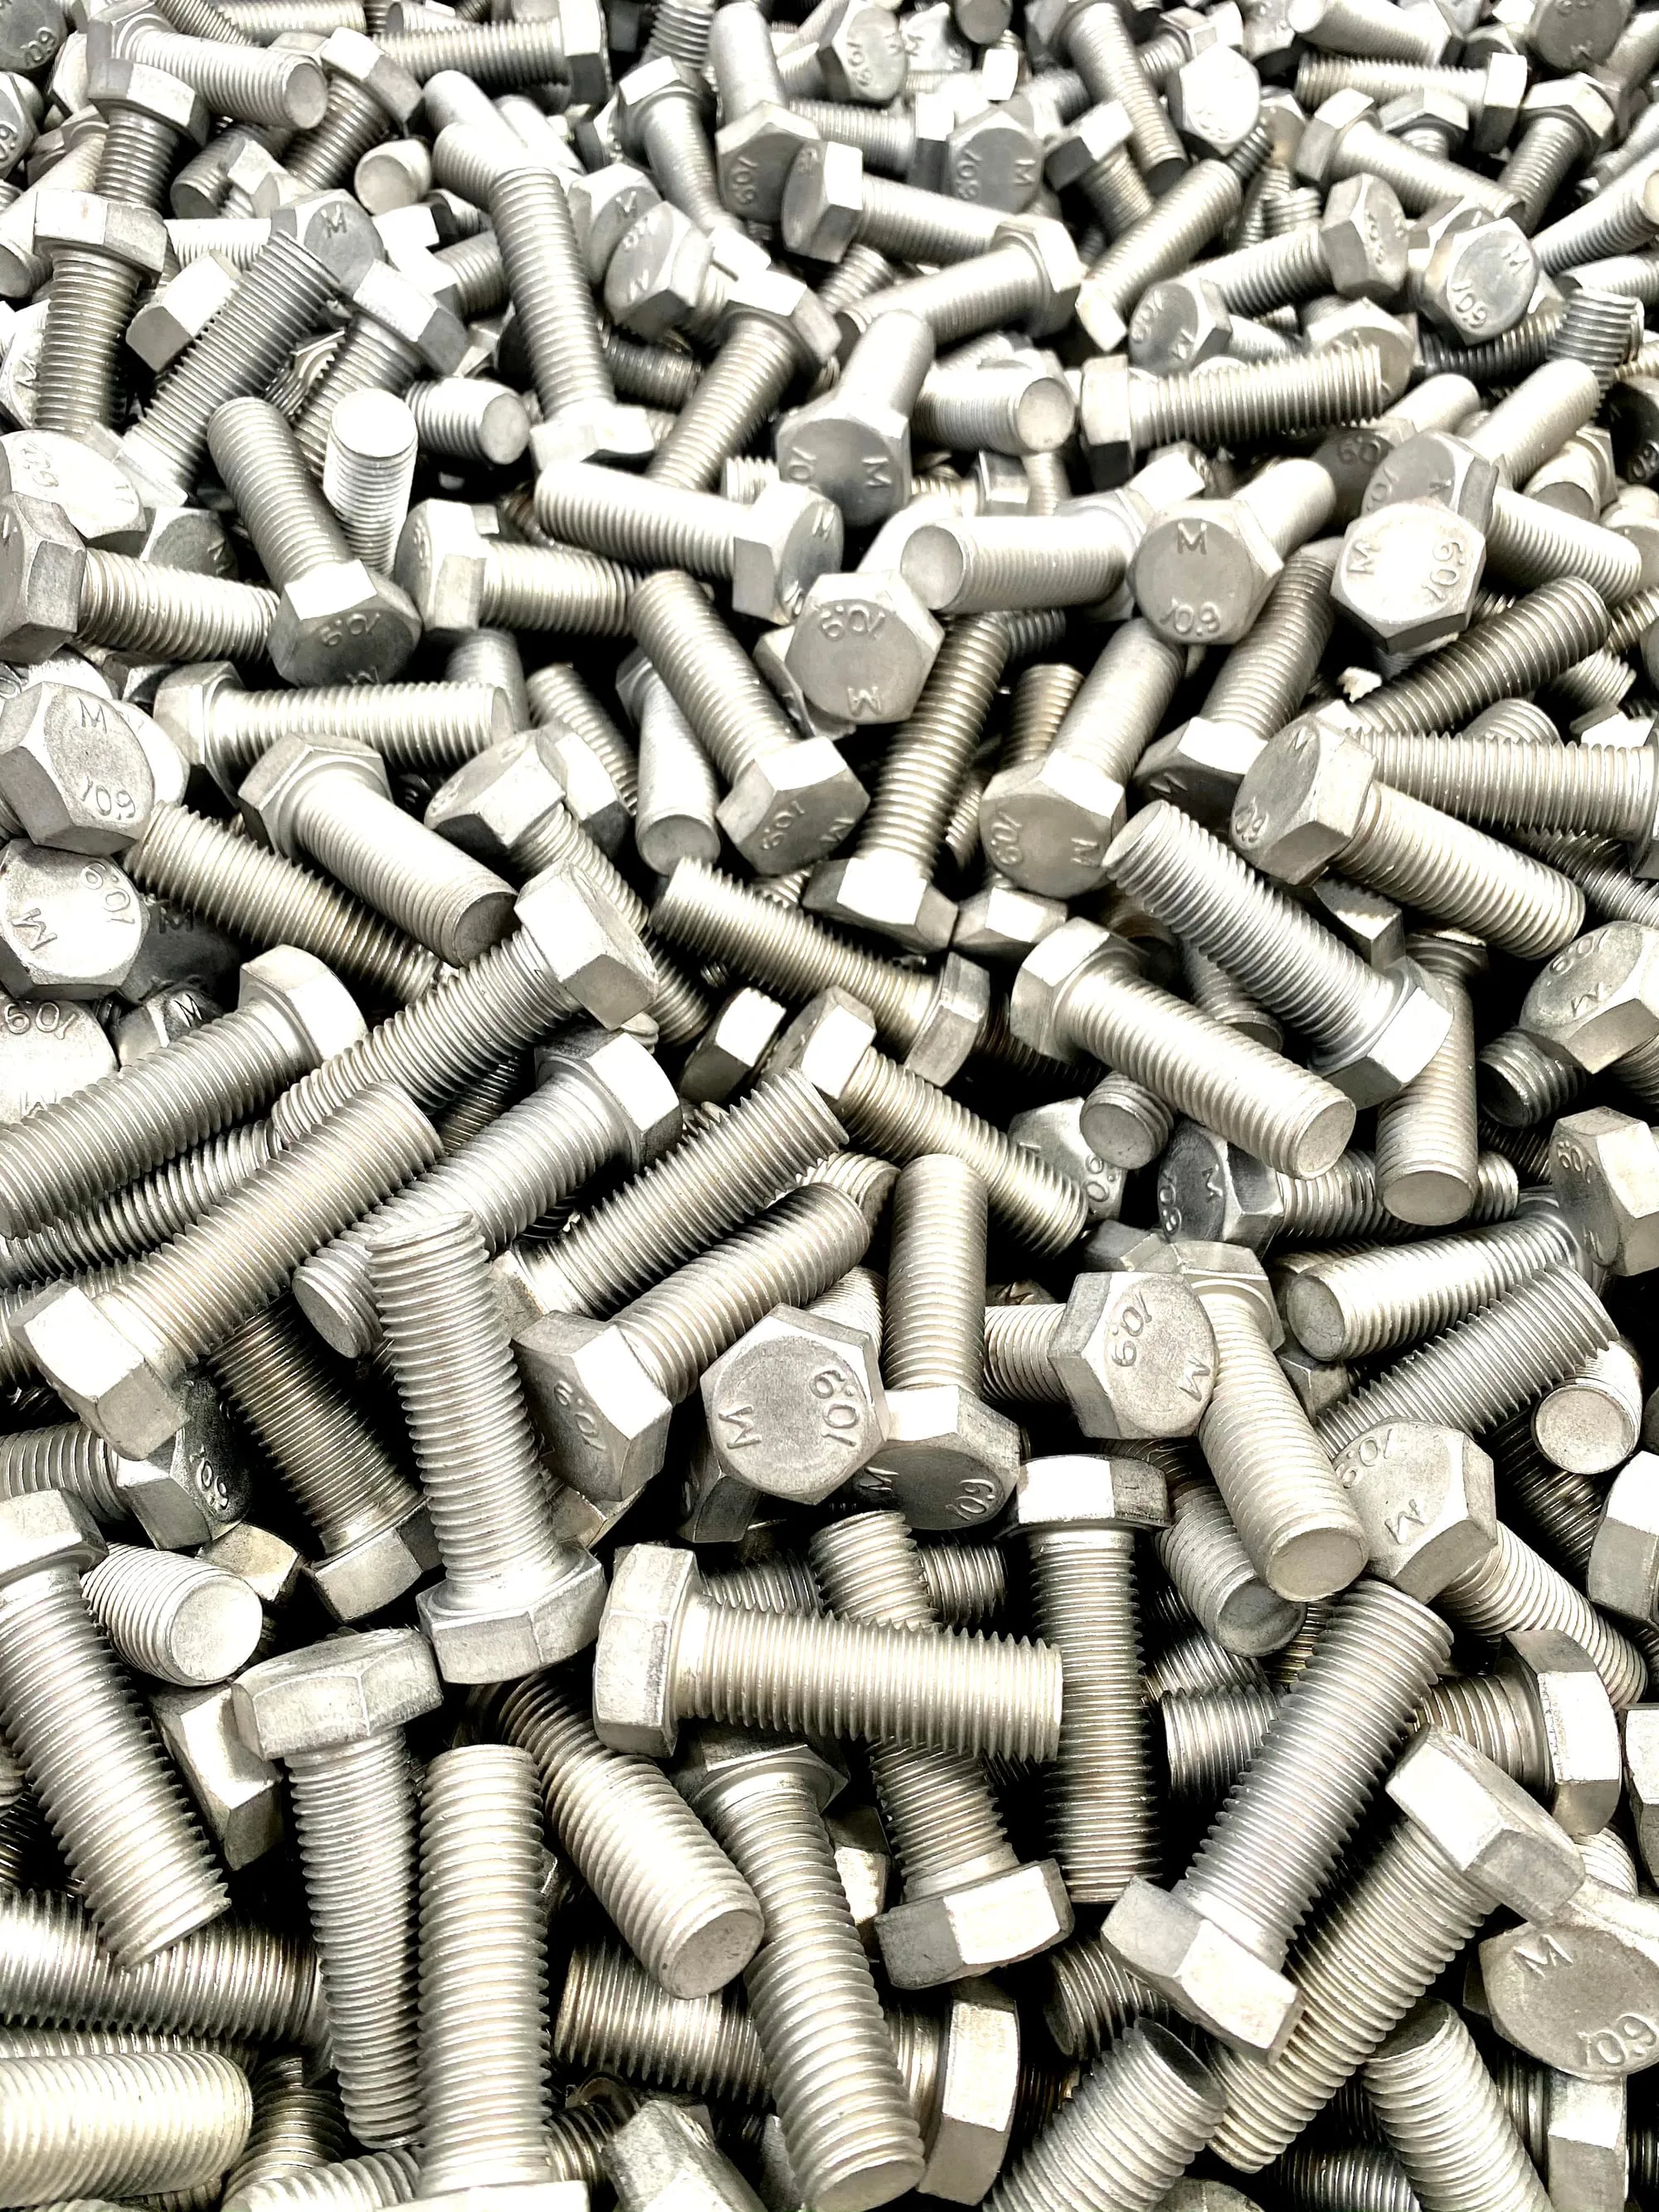
Bolts, nuts and module-mounting clips, in ground-mount plants and on roofs — cheap parts whose replacement means mobilizing crew and equipment.
Structure and profile
Support and tracker components, exposed to weather for the whole life of the asset.
Coastal environment
Plants near the sea, where salt spray is permanent and ordinary zinc does not hold up to the project horizon.
Heavy-vehicle supply chain
The same line meets OEM specifications in the segment — among them Mercedes-Benz and Scania.
What specifiers usually ask.
Why use zinc-nickel on solar structure instead of ordinary zinc?
Because the asset’s horizon is decades and replacing the fastener costs far more than the fastener. Electrolytic zinc sits between 200 and 300 hours of salt spray; the zinc-nickel base runs from 900 to 1,000 h, and the controlled process reaches 1,500 h. The calculation that matters is the cost of going back up on the roof.
What secures the 1,500 hours in practice?
Process control, not final inspection. The alloy is measured by X-ray fluorescence during production, the bath temperature is tracked and the sealer is applied to specification. A coating with an out-of-range alloy looks the same and does not get there.