Zinc-nickel plating
Zinc-nickel to ASTM B841 and ISO 4042, with a 12 to 16% nickel alloy and resistance above 1,000 hours of salt spray, controlled by X-ray.
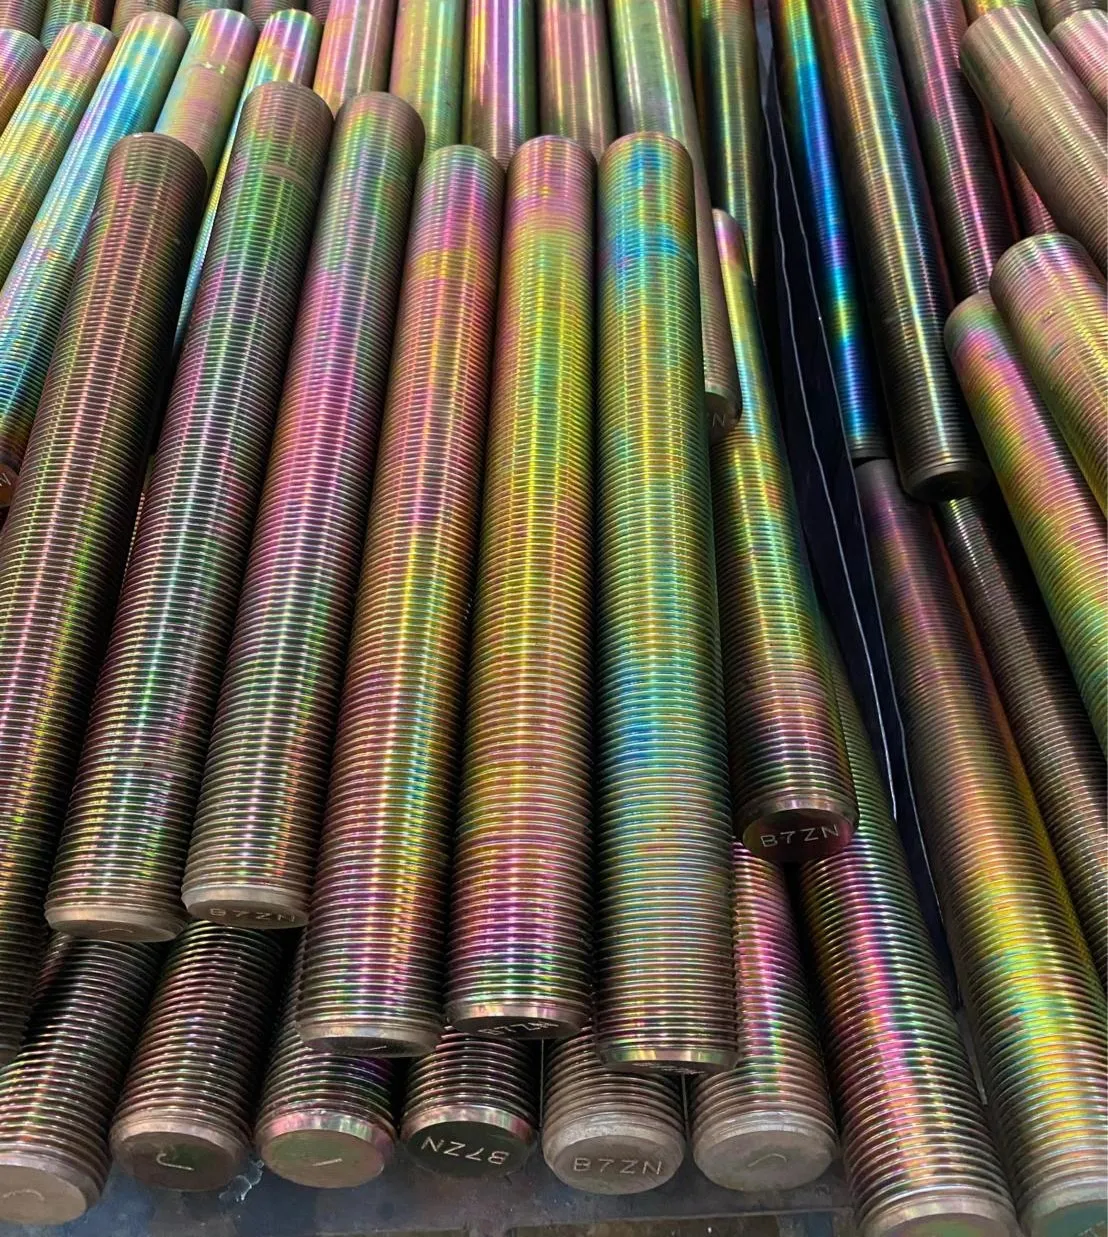
The layers are stress-free, ductile and highly penetrating — they cover deeply profiled parts well, in a rotating barrel as on a rack. It accepts white, black or clear trivalent passivation with no loss of protection. ISO 4042:2022 is today one of the most relevant standards for fastener coating, and it is what sets the 12 to 16% alloy. We meet different balances according to the customer’s specification.
Hexavalent chromium passivation. It was a leap of an order of magnitude over zinc.
Throwing power is what separates zinc-nickel from ordinary zinc in practice: it covers well across practically the whole current-density range, so a deeply profiled part, a blind hole or a recess gets a layer where zinc would leave a weak region. That is why the same bath serves rotating barrel and rack.
The alloy decides the result, and it cannot be seen. Outside the 12 to 16% nickel range the coating looks compliant and fails in the field — appearance, color and thickness stay the same. That is why the alloy is measured by X-ray fluorescence during the process, not only at final inspection. When choosing a supplier, it is the question worth asking: is the X-ray calibrated and is the alloy tracked in process?
For high-hardness fasteners, zinc-nickel does not travel alone. The hydrogen generated in electrodeposition diffuses into the metal, and relief has to follow right after the bath, in an oven with a surveyed uniformity — that is what hydrogen embrittlement relief solves, and what the audit checks.
Technical data
- Alloy
- 12 to 16% nickel — controlled by XRF
- Thickness (O&G practice)
- 10 µm
- Salt spray
- > 1,000 h
- Main standard
- ASTM B841 · classes 1 and 2, grade 10 B+E
- Passivation
- White, black or clear trivalent
- Equipment
- Rotating barrel and rack
- Process supplier
- MacDermid
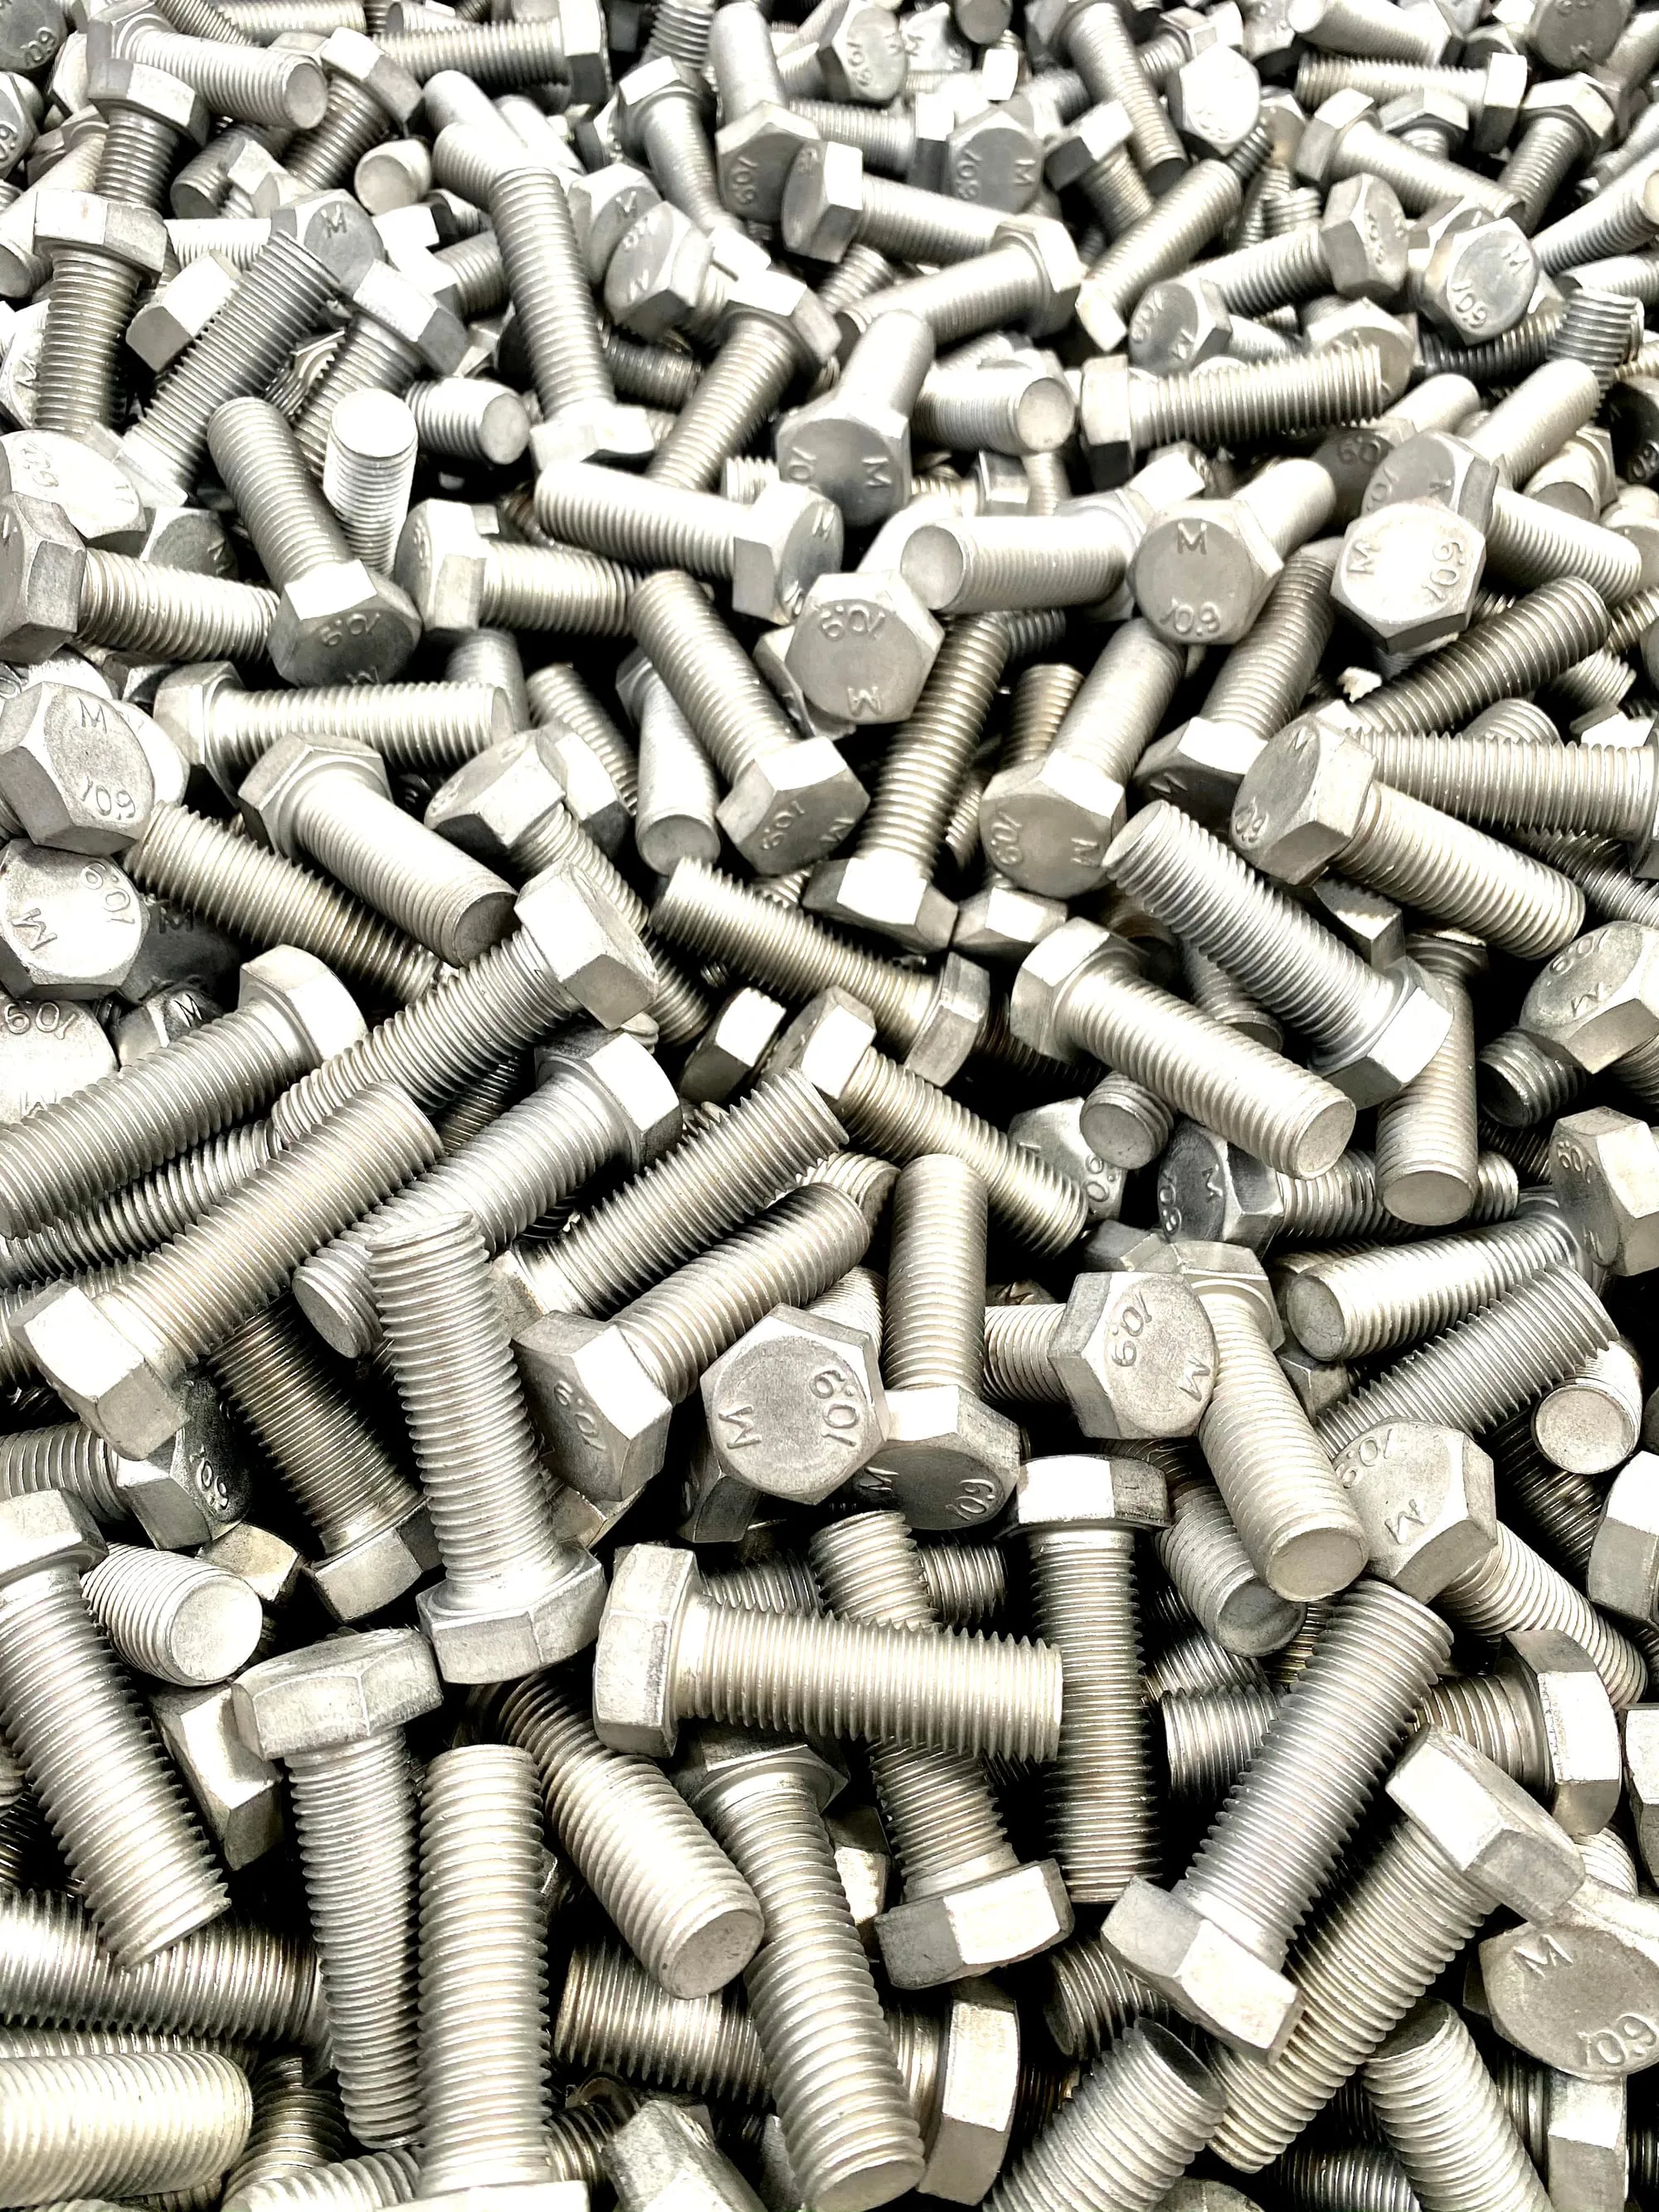
What each standard sets for Zinc-nickel.
The chip at the top of the page names the standard. This table says what it requires — which is what the specifier checks before closing the drawing.
| Standard | What it covers | What it sets here |
|---|---|---|
| ASTM B841 | Coating specification | The standard for electrodeposited zinc-nickel. It sets class, grade and type of passivation — it is the one the full designation cites. |
| ISO 4042:2022 | Fastener coating | The fourth edition, of 2022, is the current reference for fasteners: it sets the alloy at 12 to 16% nickel and covers trivalent passivations. |
| ISO 15726 | Electrodeposited zinc alloy | Requirements for zinc alloy with nickel, iron or cobalt on iron and steel. |
| DIN 50979 | Automotive system | The umbrella standard of the European automotive industry for zinc and zinc-alloy coating, with passivation and sealer. |
| Fiat PS50031 | Automaker specification | Zinc-nickel coating for vehicle components. |
| Petrobras N-215 | Operator specification | Zinc, zinc-nickel and PTFE on oil and gas components. |
| ASTM B117 | Test method | Neutral salt spray. It is a TEST method, not a coating specification — the two appear together because one proves the other. |
The applications that come here.
Oil & gas and subsea
Flange studs, nuts, stud bolts and valve components, usually with a fluoropolymer finish on top to add friction control.
Automotive
Chassis, suspension and engine fasteners, stamped parts and under-hood components — where trivalent passivation replaced hexavalent chromium without losing protection.
Solar energy
Fasteners and structure for photovoltaic panels, exposed to the weather for decades, where replacing one bolt costs far more than the bolt.
Wind and infrastructure
Large components in an aggressive atmosphere, with the alloy balanced to the customer’s specification.
In a combined system, performance does not add up — it multiplies.
The zinc-nickel system with a fluoropolymer finish for oil and gas has its own page, with the full ASTM B841 designation, the friction argument and what the test hours do not say — see the Zn-Ni + PTFE system.
| Metallic base | Organic layer | Salt spray | Remarks |
|---|---|---|---|
| Zinc-nickel | PTFE Sapucaia | over 3,500 h independent external laboratory | The best-selling oil and gas system in the line. Tested at an independent external laboratory contracted by Sapucaia. |
| Zinc-nickel | Xylan® 1070 · solvent-based · 16 µm | over 3,500 h Sapucaia technical data | Working range from −195 °C to 260 °C — the widest in the line. More than three and a half times zinc-nickel alone, with friction control added. |
| Zinc-nickel | Xylan® 1424 · water-based · 16 µm | over 3,500 h performance specified by Sapucaia | Working range from −20 °C to 180 °C. Water-based, for process components where the chemical inertness of the fluoropolymer is the requirement. |
Variations of this line.
White trivalent zinc-nickel
The most requested finish in the line: white trivalent passivation, free of hexavalent chromium, with 1,000 hours of salt spray and the test report sent on request.
Black zinc-nickel
A uniform black finish without giving up protection — the same controlled zinc-nickel alloy, with black trivalent passivation and sealer. It is a different coating from black zinc.
Zinc-nickel for solar energy
Panel structure spends 25 years outdoors, with fasteners nobody will replace. The controlled process reaches 1,500 hours of salt spray.
What specifiers usually ask.
I specified ASTM B841 grade 10. What if I need more resistance?
It is the same deposited zinc-nickel — the layer structure changes, not the material. Nanostructured zinc-nickel, under specification ASTM B1025-25, is what we apply as NanoGalv®: from 10 µm the Modumetal test in ASTM B117 records over 10,000 hours to red rust. The part, the thread and the design do not change — the line it is processed on does. Send the drawing and the standard of your end customer and our sales team returns the full designation.
What is the correct zinc-nickel alloy?
From 12 to 16% nickel, the range set by ISO 4042:2022. Below that the coating loses much of its corrosion resistance; above it, it becomes brittle and adhesion suffers. Because the difference does not show in the appearance of the part, the alloy is measured by X-ray fluorescence during the process.
Can zinc-nickel be passivated in any color?
Yes — white, black or clear, in trivalent passivation, with no loss of protection. Color is a choice of visual identification and of customer specification, not a performance indicator: protection comes from the alloy, the thickness and the sealer.
How many hours of salt spray does zinc-nickel withstand?
The base alone sits between 900 and 1,000 hours to red rust. With passivation and sealer, the white trivalent finish reaches 1,000 hours in test. With a fluoropolymer finish on top, the system is above 3,500 hours with any of the top coats in the line. Every hour published here comes with thickness, system and data source.
Is zinc-nickel suitable for a part that will be painted?
It is, and it is one of the most used combinations in oil and gas. The metallic layer gives sacrificial galvanic protection and the organic layer gives a chemical barrier and friction control. In that case the system does not carry the finishing passivation — where an organic layer goes on, the designation changes.
Is hydrogen embrittlement relief needed after zinc-nickel?
For high-hardness fasteners, yes, immediately after the bath. Electrodeposition generates hydrogen that diffuses into the steel; without thermal relief between 150 °C and 250 °C the part can embrittle and fail under load, sometimes weeks after assembly.